APPLICATION CASE / 01
Five-axis machining-centre workholding
Fixtures remain clamped during cutting, then release the workpiece for unloading.
China · 成都市林翔机械设备有限公司 (Chengdu Linxiang Machinery Equipment)
- Company-reported electricity saving
- 94.1%
- Holding time
- 150–300 s
- Recorded pressure
- 3.2 MPa
- Production test
- 72 h
Original equipment and duty
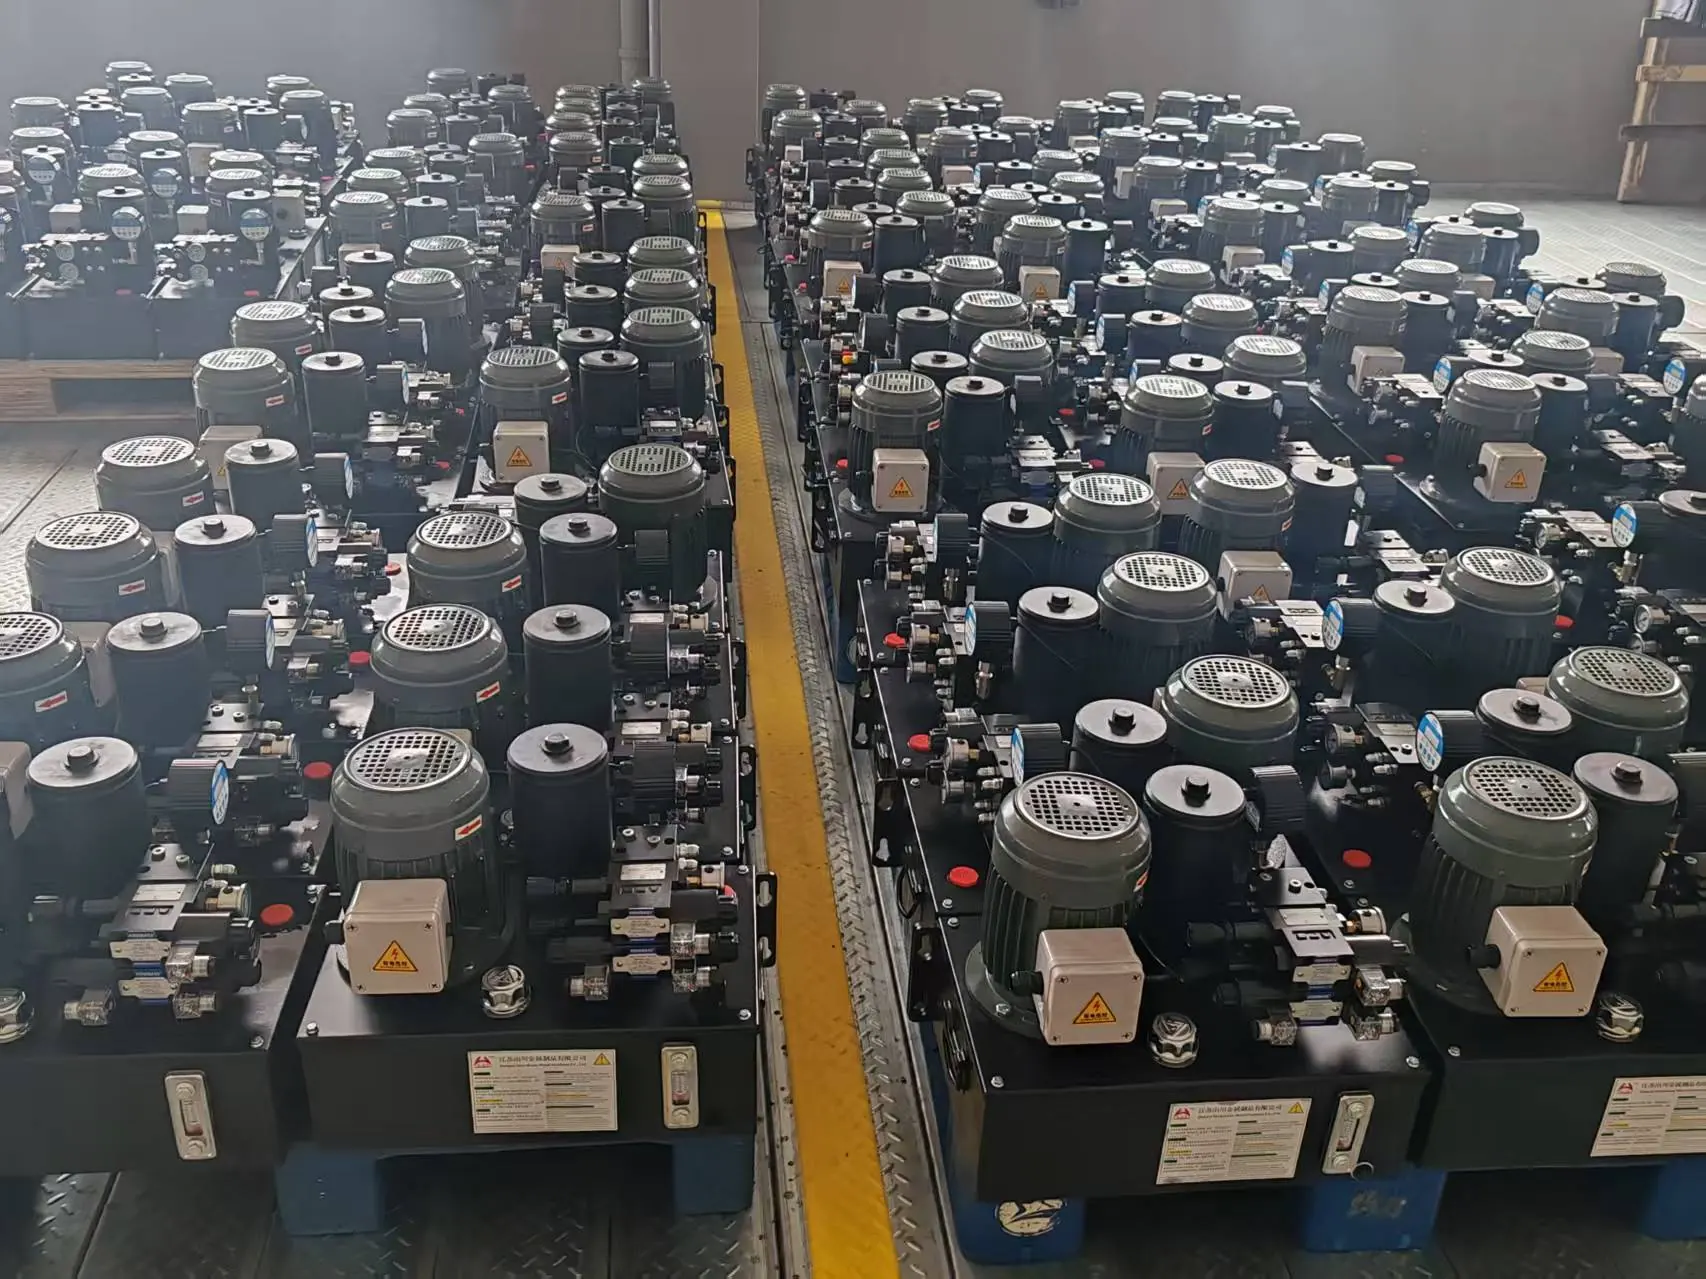
The original fixed-displacement pump ran continuously with a cooling fan. Operation showed oil temperatures of 54–61°C and noise of 77–81 dB, with seal ageing and service approximately every seven months. The machining cycle was 360 s, including 150–300 s of holding.
Project duty: 150–300 s holding time; 3.2 MPa system pressure.
02 / ON-DEMAND POWER
Power for motion. Less energy during holding.
The retrofit retained the cylinders and valve block, using a standard motor, PLC pressure feedback and an accumulator. The motor stopped after clamping pressure was established and restarted below the set threshold. The case scheme removed the original cooling fan.
- 01
Build pressure
Run the motor for clamping or pressing
- 02
Hold pressure
Stop the motor at the set pressure
- 03
Recharge as needed
Restart at the lower threshold
Test conditions and results
The project test covered 72 hours of full production on the same machine and workpiece batch, at 26–33°C ambient temperature and 3.2 MPa system pressure.
What changed after the retrofit
Reported electricity saving 94.1%
Case record date: 2025-05-12
Test record and customer feedback
Test duration / ambient temperature / pressure: 72 h · 26–33°C · 3.2 MPa
Oil temperature (before→after): 57 → 33–37°C
Noise: 79→41 dB; reported oil-change interval: 7→14 months.
Acceptance on the first review and fitment to subsequent new machining centres.
Customer feedback
The motor stops during standby. The station no longer generates heat continuously or needs a cooling fan. Energy savings exceeded expectations, stable pressure supports precision machining, and standard parts simplify repairs.
Selection checks for a similar duty
The described retrofit retains the cylinders and valve block and uses intermittent holding. Review allowed pressure drop, clamping response and internal leakage.
Explore the solution for this duty →
Cooler removal, maintenance intervals and energy results relate only to this case record. Confirm heat balance, allowed pressure drop, leakage and duty rating for each new project.